

Precision Sugar Refining &
Industrial Ethanol Distillery
Serving domestic and international markets across food, beverage, pharmaceutical and industrial applications.
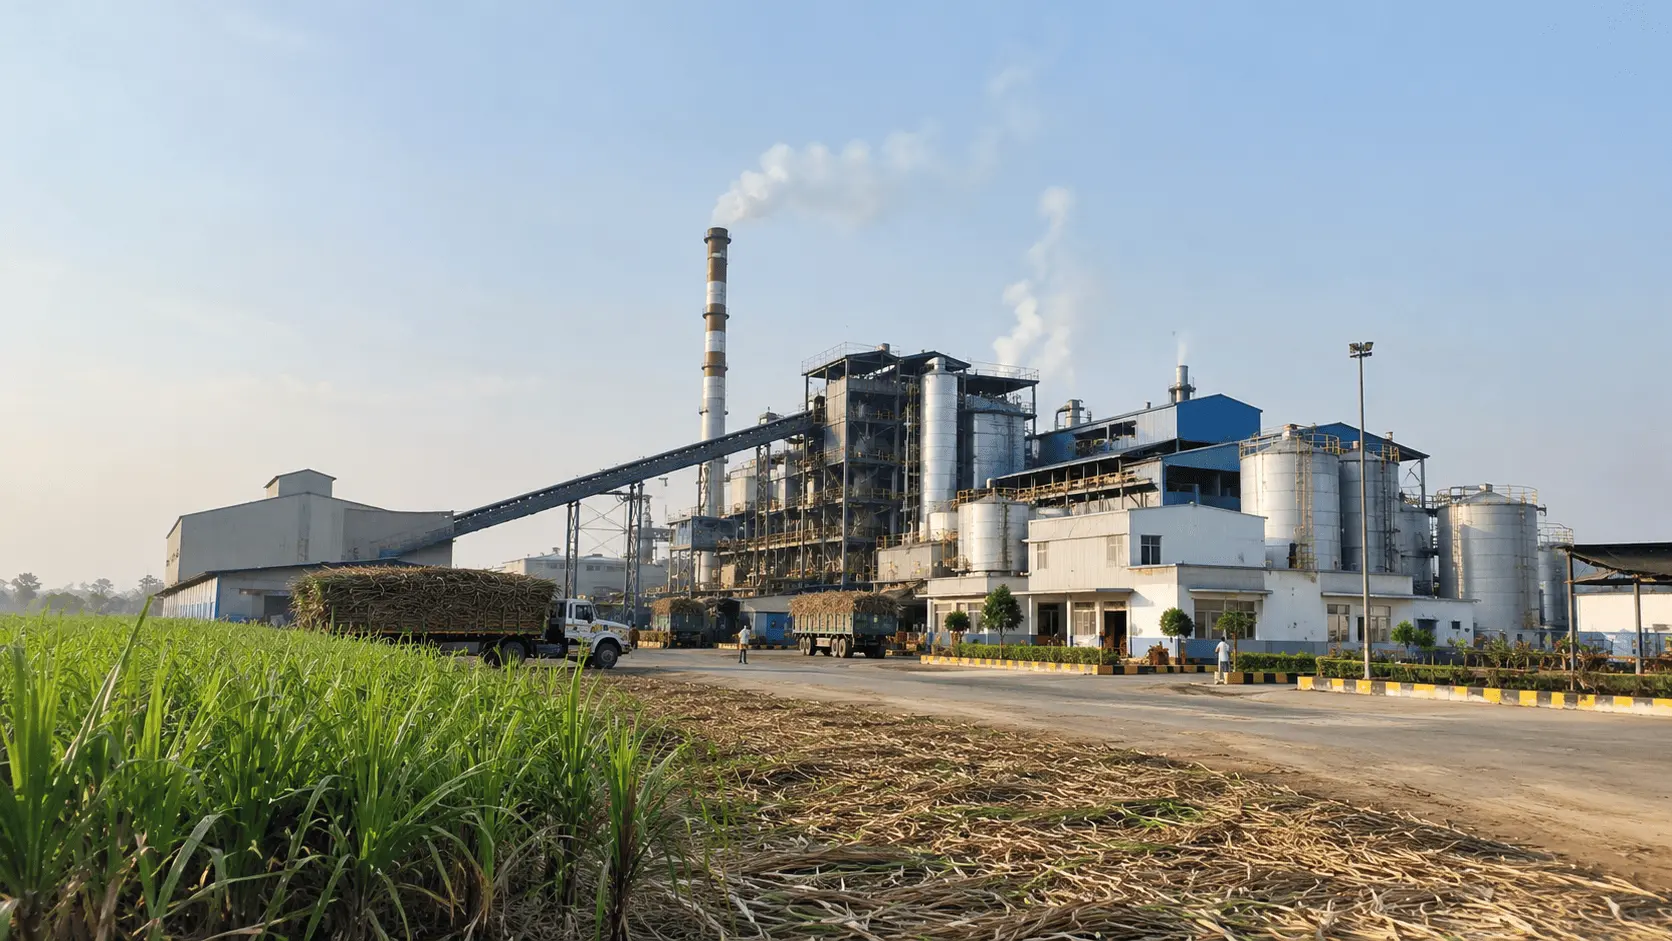
HAAF OPERATION
Industry Benchmarks
99.98%
Crystalline Sugar Purity
Exceeding stringent pharmacopeia IP/BP standards.
8,000 MT
Daily Crushing Capacity
2025–2026 Benchmark | 960K MT Annual Capacity
73M Liters
Annual Ethanol Production
Food-grade and industrial-grade ethanol capacity.
Integrated Quality & Supply Chain Control
We engineer our refining processes to guarantee the highest grade sucrose and bio-ethanol products globally. Our state-of-the-art facilities manage the full sugar grade range from pharmaceutical and beverage-specific formulations, down to high-volume commercial and custom specialty consumer lines.
In tandem with our sugar operations, our integrated distillery repurposes molasses byproducts to manufacture premium Extra Neutral Alcohol (ENA) and heavy-duty industrial fuel bio-ethanol, driving complete resource circularity.
Sugar & Distilled Product Portfolio
Pharma & Beverage Sugar Refining
Ultra-pure sucrose engineered specifically for medical formulations, pharmaceutical excipients, and high-standard beverage sweetening.
- Meets BP / USP specs
- Low-ash crystalline sucrose
- Consistent turbidity levels
Commercial & Bulk Industrial Supply
Scalable packaging and high-volume industrial shipping models of premium standard sugar grades tailored for food manufacturing partners.
- Multi-ton packaging formats
- Stable logistics lines
- All-season supply guarantees
Specialty Lines & Retail Packaging
Tailored crystalline sizes, custom demerara, confectioners sugar, and bespoke retail packages ready for automated co-packing.
- Custom grain dimensions
- FSSC 22000 certified
- Private labeling options
Integrated ENA & Industrial Ethanol
High purity Extra Neutral Alcohol (ENA) at 96% ABV for premium beverage distillation, cosmetic applications, and chemical synthesis.
- Beverage grade ENA
- Cosmetic formulation ready
- Strict organoleptic testing
Fuel Bio-Ethanol Distillery Operations
High-performance anhydrous and hydrous bio-ethanol designed to meet clean-energy mandates and industrial solvent parameters.
- Anhydrous 99.8% purity
- Eco-friendly fuel blending
- Global transport spec compliance
Molasses Valorization & Cogeneration
Direct thermal energy conversion utilizing fibrous cane residue and organic molasses valorization loops to power self-sufficient processing facilities.
- 100% steam grid recycling
- Carbon reduction programs
- Organic organic fertilizer byproducts
Quality & Distillery Workflow
01
Cane Intake
Incoming raw cane receives real-time sucrose-level and moisture analytics.
Automated sampling within 10 minutes of arrival.
02
Fermentation
Molasses byproducts undergo controlled fermentation.
Proprietary yeast strains maximize ABV conversion.
03
Lab QA
Crystalline sugar and distilled liquids endure rigorous chromatography profiling.
Certified ISO 17025 laboratory verification.
04
Logistics
Direct bulk pipeline loading into heavy stainless steel chemical tank fleet.
Fully sealed, tracked global shipping vectors.
Need Custom Sugar Specs
or Ethanol Supply?
Our industrial engineering and logistics teams are ready to custom-formulate sugar grain sizes, liquid syrup parameters, or distillation specs to fit your assembly line.